China INNOMOTICS Speed Reducers Factory Offers Advanced Drive Technology for Global Industries
2026-09-25
Speed reducers rarely make headlines, but they sit at the heart of nearly every automated process. When a Chinese factory starts shipping INNOMOTICS-class drive technology to global industries, it’s worth pausing to look under the hood. Chuangjuman is that factory—and its approach to speed reducer design is already changing how engineers think about torque, precision, and uptime. Here’s what you need to know before your next drive system decision.
The Unseen Workhorse: How INNOMOTICS Speed Reducers Keep Global Industry Moving
In the guts of a port crane swinging forty-ton containers over a dock, or buried inside a food processor that runs eighteen hours a day without a break, there is a component nobody talks about. INNOMOTICS speed reducers do the kind of heavy lifting that rarely makes headlines. They step down motor speeds, multiply torque, and absorb the shock loads that would shatter lesser gearboxes. Their work is unglamorous, precise, and absolutely essential.
What sets these reducers apart is not a single breakthrough but a stubborn refusal to fail. Mining conveyor systems in Chilean copper mines, automotive assembly lines in Stuttgart, wastewater treatment plants in Singapore—each one depends on a gear train that has to mesh perfectly under heat, dust, and constant vibration. INNOMOTICS designs for that reality, using case-hardened gears, optimized tooth profiles, and labyrinth seals that keep out the grit that kills ordinary equipment.
The result is a kind of industrial quietness. When a speed reducer works, nobody notices. When it stops, an entire production line stops with it. That is why plant engineers across six continents keep specifying INNOMOTICS—not for the name on the housing, but for the thousand shifts it will survive without a second thought.
Engineering Precision: Inside the Manufacturing Process of INNOMOTICS Drives
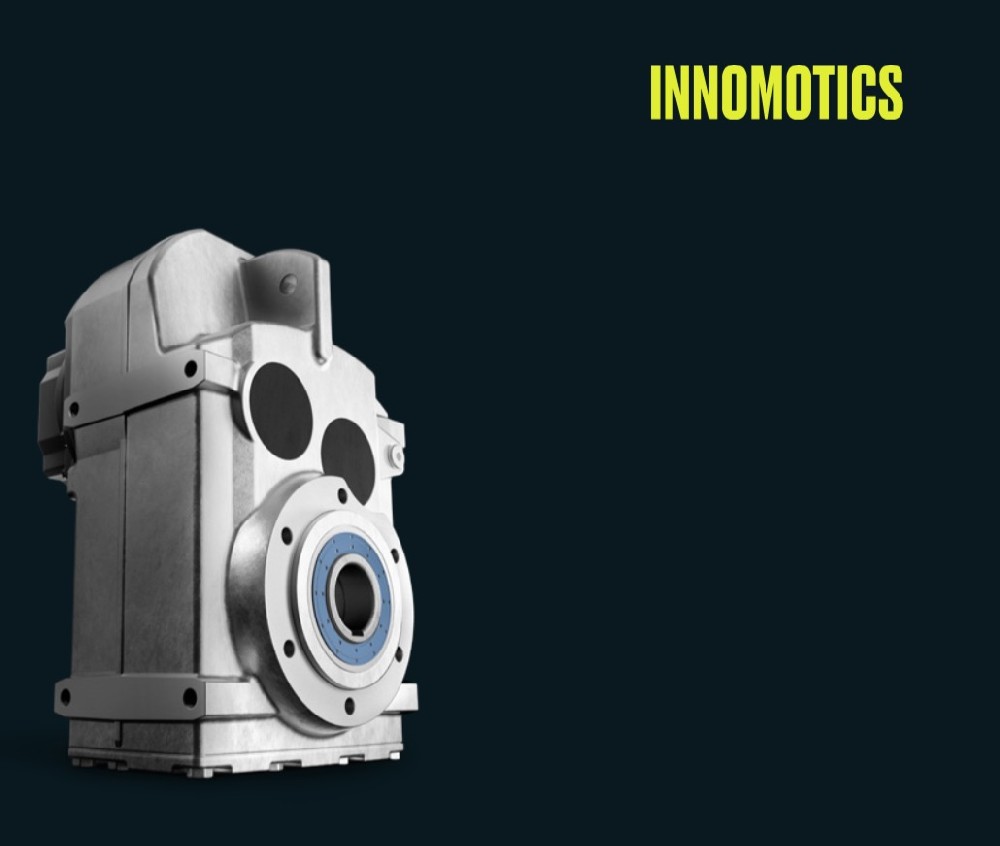
At INNOMOTICS, precision begins long before the first component is cut. Raw castings and forgings enter a climate-controlled machining hall where five-axis CNC centers hold tolerances down to ±3 microns—about a tenth the width of a human hair. Each batch is tracked with a digital twin, so if a spindle drifts by even a fraction, the system flags it before a single out-of-spec part reaches assembly.
The assembly line is a study in controlled repetition. Robots apply torque to bolt patterns within 0.5 N·m of target, while laser sensors check rotor-to-stator air gaps on every unit. Technicians don’t just rely on automated checks; they perform tactile inspections—running a gloved finger along gear teeth to catch micro-burrs that optical scanners might miss. It’s this blend of metrology and human judgment that keeps scrap rates below 0.2%.
Before any drive leaves the facility, it endures a brutal final exam. Motors are spun to 150% of rated speed, then thermally cycled between -20°C and 60°C while under full load. Vibration signatures are compared against a golden reference unit; deviations beyond 0.1 mm/s trigger a teardown. Only after passing a 72-hour continuous run does a drive earn its INNOMOTICS nameplate—and a serial number that traces every torque reading back to the exact tool used on line three.
From Cement Plants to Conveyor Belts: Applications of INNOMOTICS Reducers
Cement production demands relentless torque and endurance from every drive component. INNOMOTICS reducers handle the punishing loads of kiln drives, raw mill separators, and clinker coolers without flinching. Their hardened gear stages and optimized bearing arrangements shrug off dust, heat, and continuous operation, letting plant operators forget about the gearbox and focus on output quality.
Shift the scene to a sprawling conveyor network, and the same design philosophy pays off in different ways. Belt conveyors, screw conveyors, and bucket elevators all benefit from the compact footprint and high efficiency of these units. Sudden load spikes from uneven material feed get absorbed smoothly, protecting belts and couplings from shock damage. Maintenance crews appreciate the easy access to oil fill and drain points, cutting routine service interruptions to a fraction of typical downtime.
What ties these applications together is a quiet confidence in the drivetrain. INNOMOTICS reducers don't just survive harsh environments—they turn them into an advantage by matching thermal capacity and sealing to real-world conditions. From the gritty air of a cement mill to the steady hum of a distribution conveyor, the result is fewer unplanned stops and a longer, more predictable service life.
Why Heavy Industry Trusts INNOMOTICS for Reliable Power Transmission
In heavy industry, downtime isn't an inconvenience—it's a financial wound that can bleed millions per hour. That reality reshapes how maintenance teams evaluate every component, especially the gearboxes and motors that keep conveyors, crushers, and kilns turning. INNOMOTICS has earned its place in these environments not through flashy claims, but through a stubborn insistence on engineering margins that leave room for the unexpected. Whether it's a sudden load spike in a steel mill or dust-laden air in a cement plant, their power transmission systems are built to absorb punishment without flinching.
What separates a trusted supplier from a transactional vendor is how they handle the moments after installation. Heavy industry operators often mention the same detail: when a drive unit does need attention, the INNOMOTICS response doesn't start with a ticket number—it starts with a conversation. Their field engineers tend to know the application, the history, and the local conditions, which means replacements or repairs happen with a clarity that generic catalogs can't provide. That kind of practical knowledge accumulates over decades of working inside mines, refineries, and foundries where failure isn't an option.
Reliability also lives in the unglamorous choices: bearing selections that favor longevity over cost, sealing systems designed for abrasive environments, and thermal management that prevents premature wear. INNOMOTICS doesn't chase the lightest weight or the lowest bid; they chase uninterrupted operation. For plant managers who measure success in quarter-century lifespans rather than quarterly reports, that philosophy translates into fewer emergency shutdowns, less overtime labor, and a power transmission partner that feels less like a supplier and more like part of the maintenance crew.
Balancing Torque and Speed: The Design Philosophy Behind INNOMOTICS Gearboxes
INNOMOTICS gearboxes start from a simple observation: torque and speed pull in opposite directions, and most drives sacrifice one to get more of the other. Instead of forcing a single-stage compromise, the design spreads the load across carefully spaced helical gear pairs. That reduces peak tooth stress while keeping the output shaft compact enough to fit tight machine envelopes. The result is a drive that holds rated torque at lower speeds without running hot, and still reaches the higher output speeds automated lines often demand.
A key part of this balance is the way the gearbox manages oil flow. Rather than relying on splash lubrication alone, the housing includes internal baffles and directed channels that move lubricant toward the mesh points under varying speeds. At low RPM, the oil film stays thick enough to prevent metal-to-metal contact; at high RPM, the same channels prevent churning losses from robbing too much power. This lets one gearbox family serve both heavy, slow conveyors and faster packaging axes without a redesign.
Material choice also plays a quieter but equally important role. Case-hardened pinions are paired with tempered wheel gears, so the smaller, faster-turning component resists wear while the larger gear absorbs shock. By tuning the surface hardness and core toughness separately, INNOMOTICS avoids the usual trade-off where a gearbox is either brittle under peak torque or wears quickly during continuous high-speed runs. That is the practical meaning of balancing torque and speed: not a single magic setting, but a set of design decisions that keep both ends of the performance curve usable.
A Global Footprint: How a China-Based Factory Serves Diverse Industrial Needs
From a single production hub in Zhejiang, the factory ships precision-machined components to assembly lines in Germany, Texas, and Osaka within the same week. This isn't a story of generic mass production—orders range from low-volume custom brackets for a Dutch robotics startup to high-quantity conveyor rollers for a Brazilian mining operator. The common thread is a flexible line setup that switches between materials, tolerances, and packaging standards without sacrificing lead time.
What makes the cross-border reach work is a deliberate mix of in-house testing and local compliance knowledge. The engineering team keeps a running library of regional certifications—CE, UL, ANSI, JIS—and updates it quarterly, not as a marketing exercise but because a midwestern U.S. client once rejected a batch over a mismatched thread gauge. That lesson turned into a pre-shipment checklist now shared with logistics partners in Rotterdam and Long Beach.
The factory's global footprint isn't defined by warehouses on every continent. It's defined by quieter things—bilingual production notes, humidity-controlled crates for sea freight to Southeast Asia, and a team that can take a 2 a.m. call from a maintenance crew in Poland without making it feel like a time-zone problem. Industrial buyers keep coming back because the plant behaves less like a distant supplier and more like a nearby extension of their own floor.
FAQ
The factory focuses on speed reducers and related drive systems built for demanding industrial operations.
They are produced in China, with production standards aligned to global industrial requirements.
Common applications include material handling, packaging, food processing, and heavy machinery where torque and speed control matter.
Yes, engineering teams work with clients to adapt gear ratios, housing designs, and mounting options to specific equipment needs.
The designs incorporate precision gearing, improved thermal management, and long service intervals to reduce downtime.
The factory provides technical documentation, responsive after-sales support, and flexible logistics for overseas delivery.
Many units are built with sealed housings and protective coatings to withstand dust, moisture, and temperature swings.
Each reducer undergoes dimensional inspection, noise testing, and load trials to confirm reliable performance.
Conclusion
Behind the steady rotation of cement kilns and the relentless movement of conveyor belts lies a component few ever see: the speed reducer. At INNOMOTICS' China factory, these gearboxes are more than machined steel—they are the result of a design philosophy that treats torque and speed not as opposing forces but as partners to be balanced with exacting precision. Each unit passes through a manufacturing process where tolerances are measured in microns, ensuring that the final drive can handle sudden load spikes without sacrificing efficiency. It is this silent reliability that keeps global industry from stalling.
The proof is in the places these reducers end up. From dusty cement plants in Southeast Asia to automated conveyor systems in European logistics hubs, INNOMOTICS drives are chosen where downtime is not an option. Heavy industry trusts the brand because the factory in China operates with a global mindset—adapting housing materials, gear ratios, and sealing designs to match regional operating conditions, whether that means high humidity, extreme cold, or abrasive particulates. Rather than offering one-size-fits-all solutions, the plant produces a range of configurations that share a common core: advanced drive technology built to outlast the machinery around it.
Contact Us
Contact Person: Jony
Email: [email protected]
Tel/WhatsApp: 086-0571-86161808
Website: https://en.hzcjm.com/